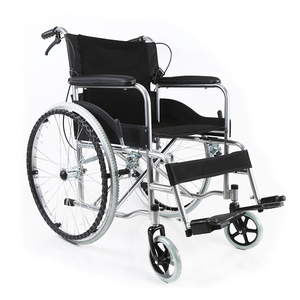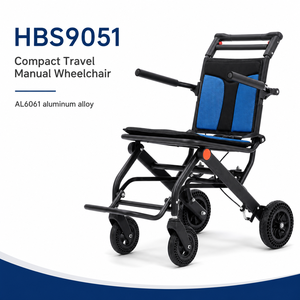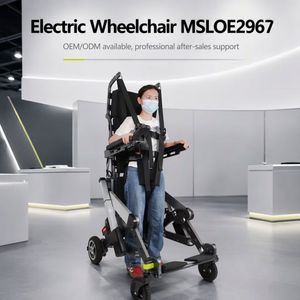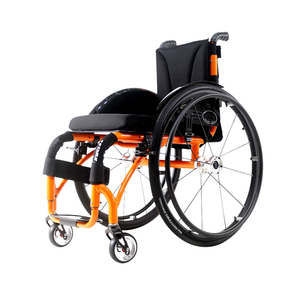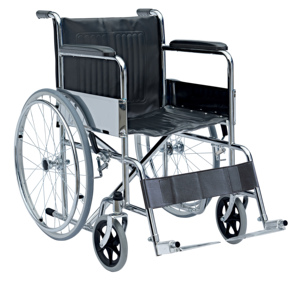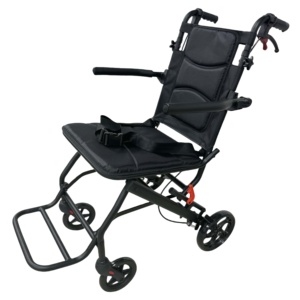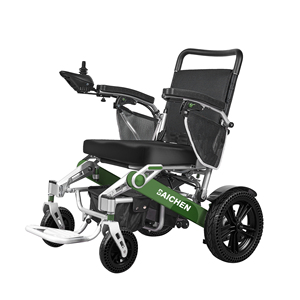
As a leading pioneer among China custom wheelchair factories and exporters, Eurogreen International Inc. (SupaMobility) operates at the intersection of medical ergonomics, advanced metallurgy, and digital power electronics. Our manufacturing philosophy centers on practical innovation, strict compliance, and precision engineering designed specifically to address the rigorous requirements of institutional distributors, healthcare procurement networks, and global mobility brands.
Our operational architecture combines decades of engineering expertise with multi-national certified facilities. Unlike generic contract manufacturers, our production lines integrate dedicated robotic welding hubs, computer-controlled stress-testing benches, and specialized battery safety simulation chambers. Every wheelchair design—from ultra-lightweight active manual frames to smart Electronic Stability Control (ESC) powerchairs—undergoes comprehensive validation before export.
Navigating global healthcare regulations requires unwavering transparency and compliance. Our manufacturing ecosystems are audited and fully certified under international quality management standards:
• ISO 13485 & ISO 9001 Certification: Full medical device quality management system implementation covering product inception, raw material verification, assembly line traceability, and post-market feedback monitoring.
• FDA Cleared & CE Marked: Compliance with US FDA requirements and EU Medical Device Regulation (MDR 2017/745), providing seamless clearance for medical device importers across North America and Europe.
• Stress Testing Protocols: Every batch undergoes dynamic roller bench load testing, multi-axis fatigue testing of frame joints, and extreme environmental thermal shock testing to ensure zero-defect field reliability.
Integrated Electronic Stability Control (ESC) dynamic braking algorithms prevent tipping on slopes and uneven terrain, automatically balancing torque output across dual brush/brushless motors.
From bespoke frame geometries and custom paint colors to specialized seat widths, joystick sensitivities, and branded packaging, we turn technical concepts into market-ready products.
Battery solutions are fully certified under UN38.3 and MSDS regulations, allowing hassle-free air cargo, maritime transport, and airline passenger travel for end-users.
The global mobility equipment industry is undergoing a structural transformation driven by demographic shifts, decentralized healthcare delivery, and rapidly evolving regulatory paradigms. Importers, clinical distributors, and government health agencies are fundamentally altering their procurement strategies. Key purchasing trends shaping the next decade include:
Traditional heavy steel wheelchairs are increasingly restricted to institutional stationary use. Global procurement is shifting decisively toward aerospace-grade aluminum (7075-T6 alloy) and carbon-fiber composite frames. B2B buyers now prioritize total unit weight (under 20kg for powerchairs) without compromising structural payload capacity (demanding 125kg to 150kg ratings). Compact quick-folding mechanisms that fit easily into compact automotive trunks have transformed from luxury features into mandatory contractual specs.
To reduce inventory holding costs and streamline replacement parts logistics, global buyers are seeking ODM factories that utilize modular component platforms. Modular designs allow distributors to swap manual wheels, power drive modules, dynamic joysticks, and therapeutic seating options onto a single standardized chassis, significantly reducing SKU complexity across regional distribution networks.
Commercial mobility equipment rental networks, municipal transport hubs, and high-end senior living facilities now demand smart wheelchairs equipped with embedded IoT modules. Fleet managers require real-time GPS tracking, remote battery health diagnostics (BMS data), automated fault alerting, and user usage telemetry to optimize maintenance schedules and minimize operational downtime.
Healthcare buyers are mitigating geopolitical risks by auditing factory resilience, raw material sourcing transparency, and ESG (Environmental, Social, and Governance) compliance. Partnering with established Chinese manufacturing hubs that maintain strict raw material testing, ethical labor standards, and traceable supply chains has become a primary prerequisite for winning government tenders.
To maintain a competitive edge, our R&D engineering divisions focus on incorporating breakthrough innovations into standardized production runs:
Next-gen electromagnetic gearless hub motors deliver 92% power conversion efficiency, whisper-quiet operation, and dynamic regenerative braking during descent.
Integration of Lithium Iron Phosphate (LiFePO4) chemistry featuring thermal runway prevention, 2000+ cycle lifespans, and fast 2-hour charging capabilities.
Anatomically contoured flame-retardant memory foam cushions paired with anti-decubitus breathable mesh to prevent pressure sores during extended use.
Whether you are seeking a turnkey OEM manufacturing partner, expanding your brand's motorized mobility catalog, or bidding on institutional healthcare contracts, our engineering team is ready to deliver.